Lightweight yet powerful, the wholesale large capacity refrigerated centrifuge continues to raise the standard for efficiency of operation. High-performance control algorithms provide instant acceleration and smooth deceleration, protecting delicate samples from stress. Dual cooling systems provide thermal stability in even long runs. Modular design provides easy maintenance and upgrading. Remote diagnostics and system optimization connectivity is available in some models. Along with these advancements, the wholesale large capacity refrigerated centrifuge becomes a bridge between traditional engineering and modern automation and functions as a pillar of accurate, high-rate separation within labs and factories around the world.

The use of wholesale large capacity refrigerated centrifuge traverses a number of scientific disciplines. In the manufacture of pharmaceuticals, it cleanses chemical compounds and removes residual unwanted matter. Biochemists employ wholesale large capacity refrigerated centrifuge in fractionating cells and isolating organelles for subsequent studies. Drink producers utilize it to filter fluids and stabilize their products. The oil and gas industries utilize wholesale large capacity refrigerated centrifuge to enhance fuel refining and clean products. {Keywords} can also be utilized in environmental analysis, aiding in the detection of pollutants in water and air samples. They are highly accurate and flexible, thus being a fundamental tool within laboratories and the manufacturing industry.
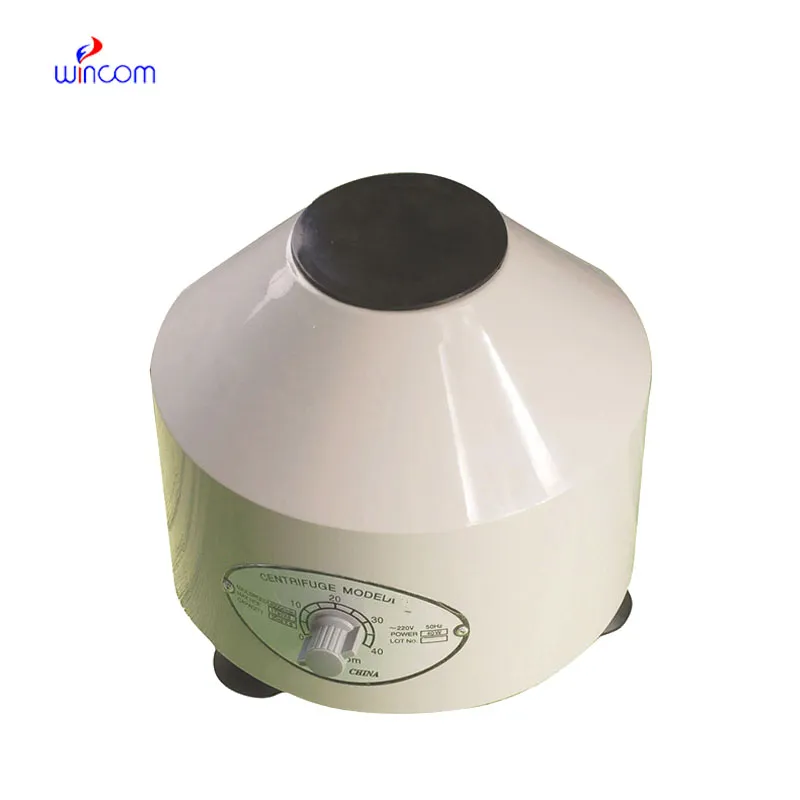
wholesale large capacity refrigerated centrifuge will integrate digital intelligence and cutting-edge engineering in the years to come. Complex algorithms will auto-tune parameters for optimum efficiency and safety. Energy-optimized designs will keep operating costs at a minimum and help support global green efforts. Robotics integration will facilitate round-the-clock unattended operation in big production setups. Modular design will provide ease of customization, allowing users to set up wholesale large capacity refrigerated centrifuge for specific scientific or industrial uses. These improvements will allow wholesale large capacity refrigerated centrifuge to not only increase performance but also establish new standards for automation, accuracy, and sustainability in the lab environments of the future.
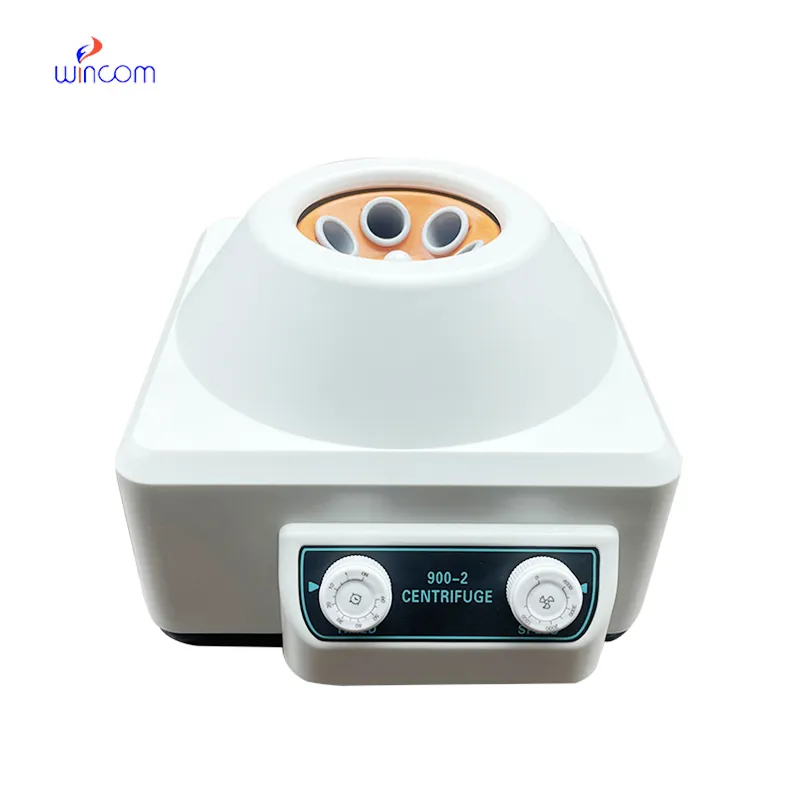
Well-maintained wholesale large capacity refrigerated centrifuge assure trouble-free operation and optimize equipment longevity. Users must ensure balanced loading to prevent excessive stress to bearings. Regular cleaning of the rotor, chamber, and seals reduces cross-contamination. Regular lubrication and calibration ensure mechanical accuracy. Logs of maintenance, checklists, and other records facilitate quality control and inspection for compliance. Internal humidity and dust exposure should be reduced. Laboratories use preventive maintenance instructions to guarantee that wholesale large capacity refrigerated centrifuge delivers constant high performance with little downtime and repair.
The wholesale large capacity refrigerated centrifuge is a staple equipment in laboratories, industries, and research facilities. Its operation is to isolate particles away from one another based on density and weight by utilizing centrifugal force. Whether examining biological fluids, purifying chemicals, or testing materials, the wholesale large capacity refrigerated centrifuge provides effective separation and purification. Advances in technology have made it faster accurate and automatic, enabling processes to be more repeatable and consistent. From clinical diagnostics to environmental analysis, wholesale large capacity refrigerated centrifuge are essential in furthering precision, productivity, and scientific innovation globally.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
This ultrasound scanner has truly improved our workflow. The image resolution and portability make it a great addition to our clinic.
The water bath performs consistently and maintains a stable temperature even during long experiments. It’s reliable and easy to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
I’d like to inquire about your x-ray machine models. Could you provide the technical datasheet, wa...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko