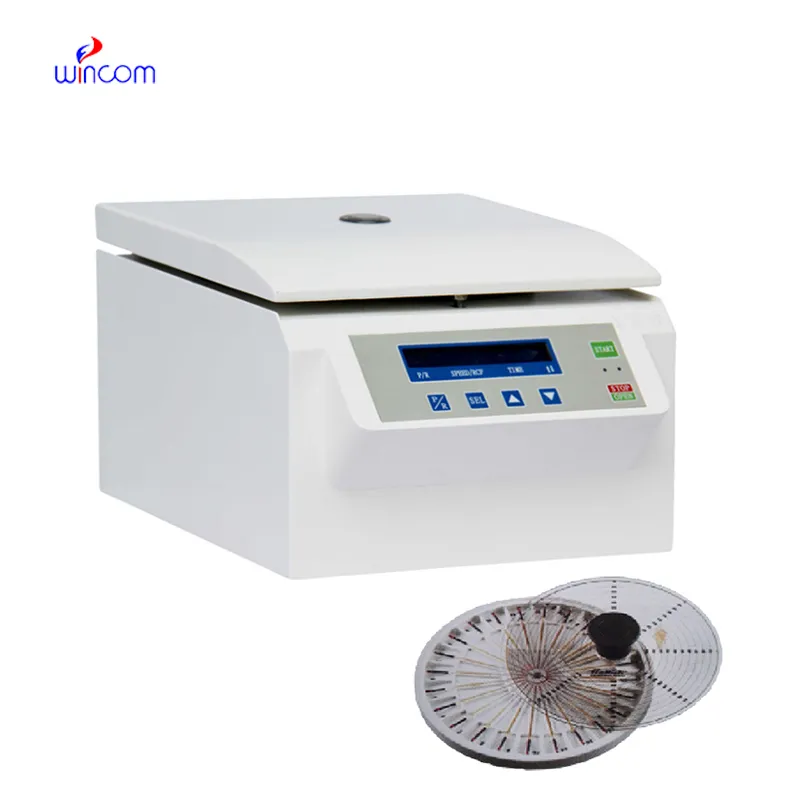
Recent innovations in super large capacity refrigerated centrifuge technology focus on the improvement of automation as well as information integration. Intelligent models now communicate with laboratory information management systems so that the recording of experimental parameters is no longer problematic. Noise reduction modules and ergonomic covers have also increased user comfort and safety. Also, controlled temperature chambers and high-speed rotors facilitate the handling of sensitive material without degradation. Such technology renders super large capacity refrigerated centrifuge equipment more adaptable to varying research needs, offering unparalled precision in particle separation and purification processes in countless industries.

super large capacity refrigerated centrifuge technology is a principal component in diverse manufacturing processes. In wastewater treatment, super large capacity refrigerated centrifuge assist in separating sludge from liquids to improve recycling efficiency. In the manufacture of cosmetics, super large capacity refrigerated centrifuge facilitate even emulsion and cream mixing. Crop research facilities apply it to analyze soil nutrients and plant extracts. It is also used in the manufacture of vaccines through the purification of viral particles and protein fractions. Through the ability to adapt to many substances and work requirements, super large capacity refrigerated centrifuge continues to support industries seeking consistency, purity, and scalability.
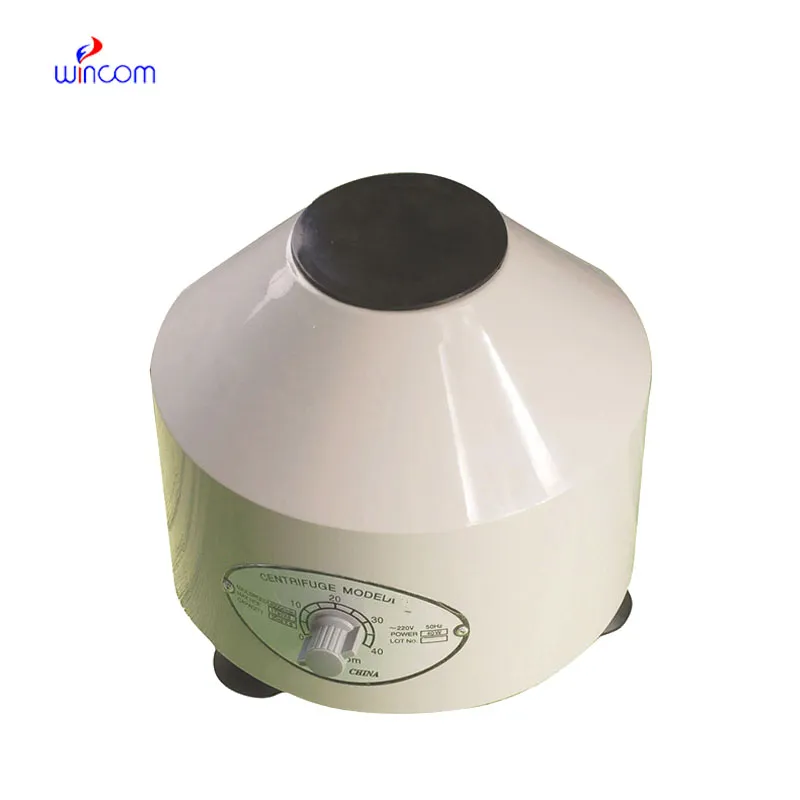
The super large capacity refrigerated centrifuge of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, super large capacity refrigerated centrifuge systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place super large capacity refrigerated centrifuge at the forefront of international scientific advancement.
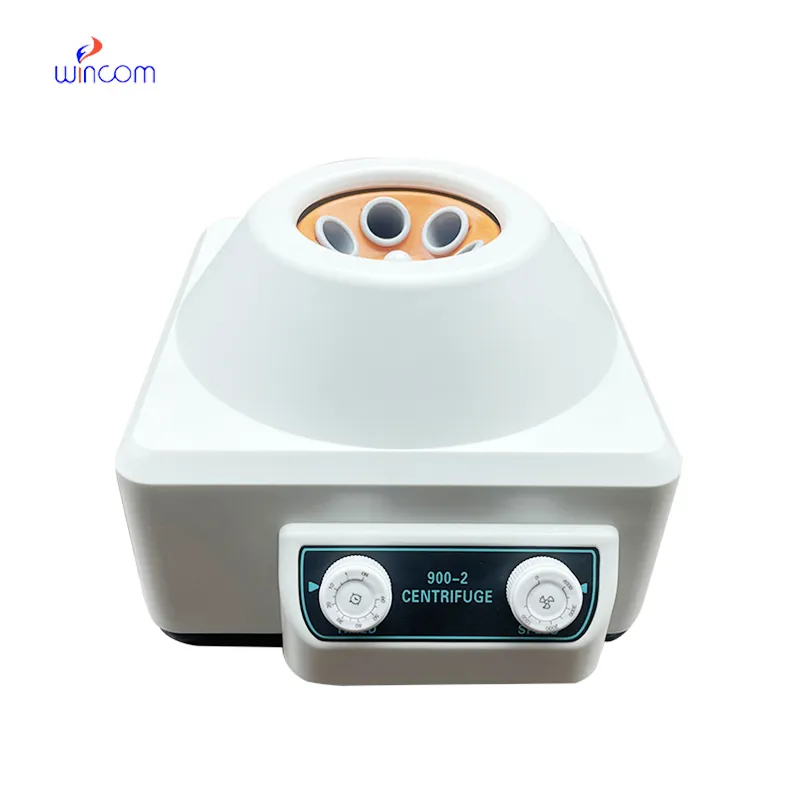
Maintenance procedure routines protect the performance and safety of super large capacity refrigerated centrifuge. The rotor needs to be visually inspected before each operation for cracks or corrosion. Mild detergents are needed for cleaning, followed by thorough drying to prevent rust. Calibration verification and vibration monitoring assist in keeping it accurate. The instrument should be set on a level surface to reduce stress on bearings. During storage, super large capacity refrigerated centrifuge must be kept covered and not plugged to keep electronics safe. Under operator discipline and regular maintenance, laboratories can offer years of trouble-free performance.
A super large capacity refrigerated centrifuge is a universal gadget designed to separate parts in a mixture through sheer spinning power. A super large capacity refrigerated centrifuge operates through the principle of sedimentation, in which heavier particles move outwards and lighter particles remain at the center. Employed within laboratories, clinics, and industry in general, a super large capacity refrigerated centrifuge may be utilized to separate materials such as blood plasma, proteins, and chemical reagents with accuracy. Modern super large capacity refrigerated centrifuge exist in various forms, from benchtop to industrial types and ultracentrifuges, all for specialized applications. They are accurate and reproducible, a necessity in production and research.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
The delivery bed is well-designed and reliable. Our staff finds it simple to operate, and patients feel comfortable using it.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
We are planning to upgrade our imaging department and would like more information on your mri machin...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko