Recent innovations in large capacity refrigerated centrifuge manufacturer technology focus on the improvement of automation as well as information integration. Intelligent models now communicate with laboratory information management systems so that the recording of experimental parameters is no longer problematic. Noise reduction modules and ergonomic covers have also increased user comfort and safety. Also, controlled temperature chambers and high-speed rotors facilitate the handling of sensitive material without degradation. Such technology renders large capacity refrigerated centrifuge manufacturer equipment more adaptable to varying research needs, offering unparalled precision in particle separation and purification processes in countless industries.

The use of large capacity refrigerated centrifuge manufacturer traverses a number of scientific disciplines. In the manufacture of pharmaceuticals, it cleanses chemical compounds and removes residual unwanted matter. Biochemists employ large capacity refrigerated centrifuge manufacturer in fractionating cells and isolating organelles for subsequent studies. Drink producers utilize it to filter fluids and stabilize their products. The oil and gas industries utilize large capacity refrigerated centrifuge manufacturer to enhance fuel refining and clean products. {Keywords} can also be utilized in environmental analysis, aiding in the detection of pollutants in water and air samples. They are highly accurate and flexible, thus being a fundamental tool within laboratories and the manufacturing industry.
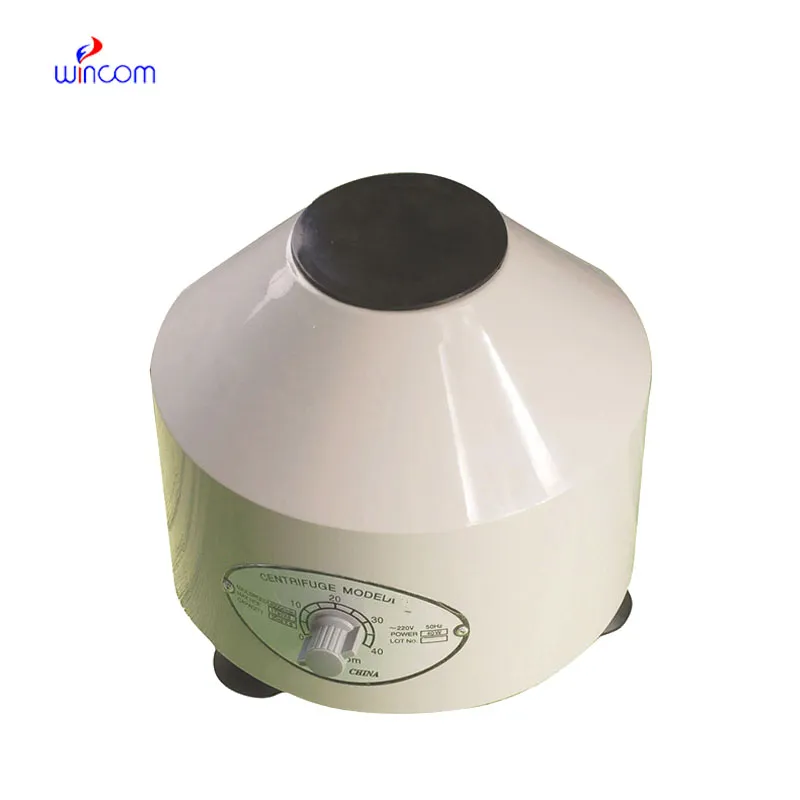
Future trends show that large capacity refrigerated centrifuge manufacturer will become more intelligent, miniaturized, and green. Researchers envision systems capable of learning for themselves and optimizing their performance from previous data results. Integration within digital laboratory workflows will render operations, from sample entry to data reporting, more seamless. Increased automation will free researchers from manual monitoring, allowing more focus on analysis. In industrial processes, large capacity refrigerated centrifuge manufacturer will have a role in cleaner production through the reduction of waste and energy usage. It is a step toward smarter scientific instrumentation that adapts to the challenges of technology.
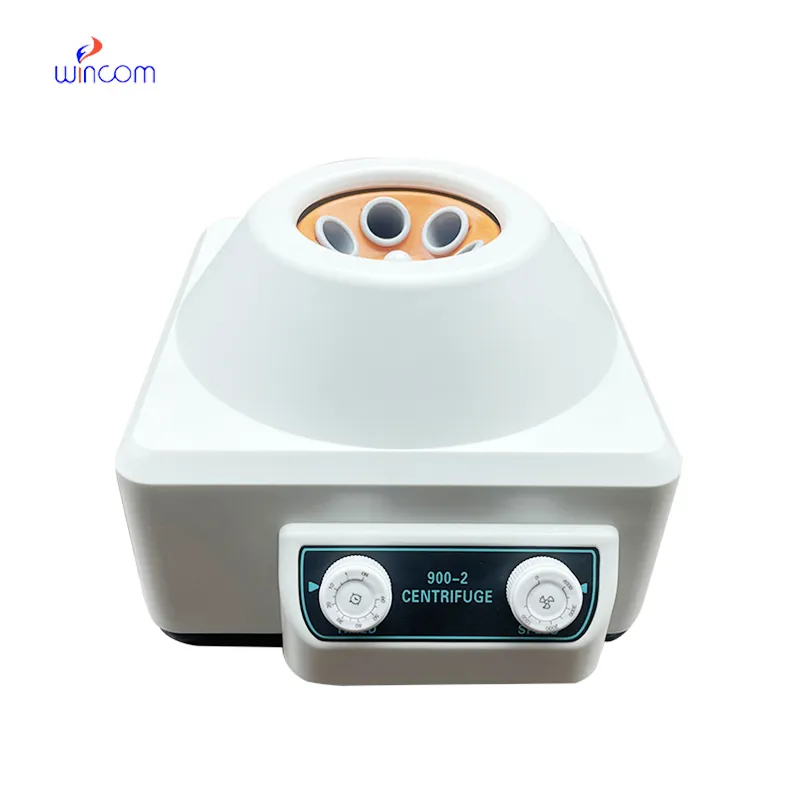
Routine maintenance of large capacity refrigerated centrifuge manufacturer begins with frequent cleaning and careful handling. Before each run, users should confirm that there are properly sealed, loaded tubes to prevent imbalance. The rotor, buckets, and seals should be washed gently and dried with air after each session. Periodic calibration checks ensure precise speed and temperature measurement. Rotor overloading is to be prevented since it will reduce motor life. With monitoring each maintenance cycle and adhering to safety protocols, laboratories can extend the functional life of large capacity refrigerated centrifuge manufacturer while ensuring precise performance.
Through controlled rotation, a large capacity refrigerated centrifuge manufacturer produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most large capacity refrigerated centrifuge manufacturer today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the large capacity refrigerated centrifuge manufacturer a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
This x-ray machine is reliable and easy to operate. Our technicians appreciate how quickly it processes scans, saving valuable time during busy patient hours.
The centrifuge operates quietly and efficiently. It’s compact but surprisingly powerful, making it perfect for daily lab use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Could you please provide more information about your microscope range? I’d like to know the magnif...
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko