Crafted specifically for precision, the large capacity refrigerated centrifuge factory is additionally improved by digital and mechanical enhancements. Intelligent balancing systems automatically eliminate unbalanced loads, improving performance as well as safety. Materials such as reinforced polymers and high-grade aluminum are becoming standard in rotor production, reducing wear and maximizing life in operation. Real-time sensors of temperature and speed offer feedback for reliable results. These developments not only improve separation efficiency but also allow for the achievement of stringent laboratory standards. With increasing research needs, large capacity refrigerated centrifuge factory technology develops further to ensure better reliability and reproducibility.

Clinical laboratory environments utilize large capacity refrigerated centrifuge factory as an important tool for proper diagnosis. Blood banks utilize it to efficiently isolate red cells, plasma, and platelets. Research laboratories employ large capacity refrigerated centrifuge factory to examine tissue samples for cellular and molecular studies. In the energy industry, it assists in the manufacture of biofuels by isolating the biomass components. Food scientists employ large capacity refrigerated centrifuge factory to reclaim fats and purify proteins while preparing products. The numerous applications reflect its capacity to enhance data reliability, process control, and yield output in a wide variety of industries and research applications.
Sustainability, connectivity, and accuracy will be the areas of future evolution of large capacity refrigerated centrifuge factory. Instruments will be made with sustainable materials and energy-efficient drives to minimize their carbon footprint. Real-time monitoring of data through cloud-based systems will facilitate real-time troubleshooting and process optimization. Portable versions will enhance accessibility in remote- or field-based studies. In pharma and biotech, large capacity refrigerated centrifuge factory will ramp up production with intelligent automation. As technology continues to evolve, large capacity refrigerated centrifuge factory will remain at the center of scientific innovation, bridging the gap between mechanical performance and digital intelligence.
Maintenance of large capacity refrigerated centrifuge factory is essential to lab safety and data integrity. Cleaning should be performed immediately following every operation, with special attention to the elimination of any liquid spills or residues from samples. The rotor should always be handled gently, placed in an upright position during storage, and never subjected to shock. Periodic inspection of lid locks and gaskets ensures airtight operation. Power cord and fuse conditions should also be checked by operators. Annual servicing by skilled technicians adds lifespan. Through regular care processes, large capacity refrigerated centrifuge factory safely and accurately continues to operate.
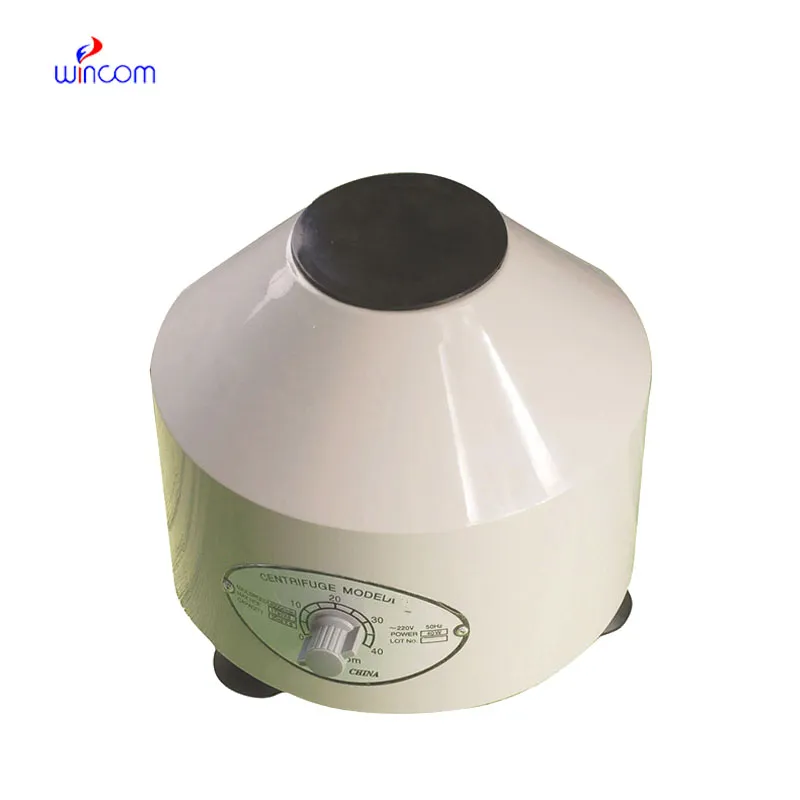
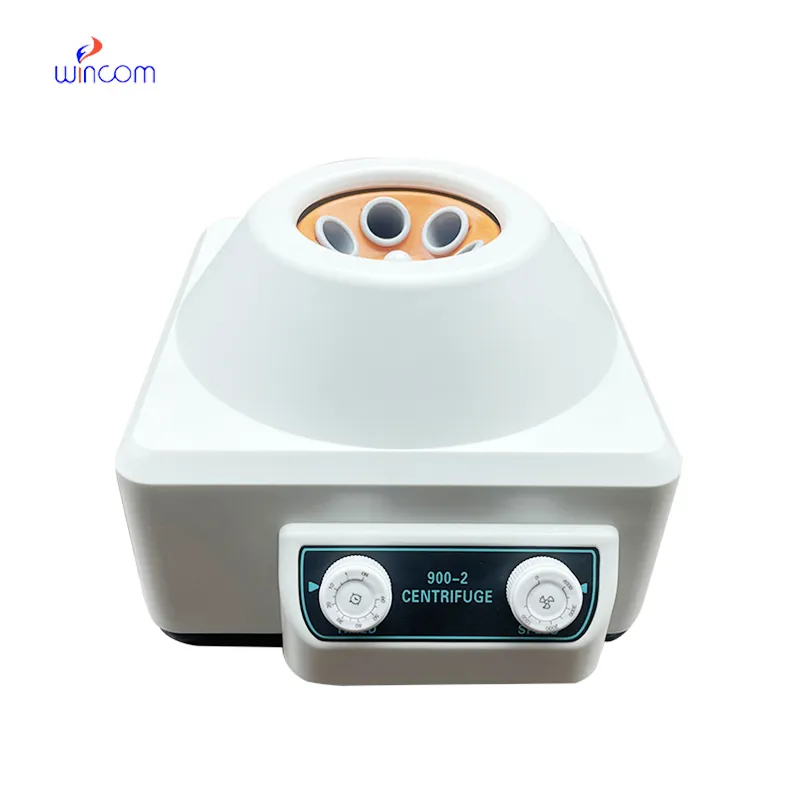
large capacity refrigerated centrifuge factory is a piece of mechanical equipment that separates simple mixtures into differentiated parts by utilizing quick spinning. It functions by employing centrifugal force, which expels heavier elements and brings lighter elements closer towards the axis. This principle makes crucial work possible in microbiology, pharmaceuticals, and materials science. High-speed models can achieve exceptional separation accuracy in mere minutes. Modern large capacity refrigerated centrifuge factory feature digital interfaces, temperature control, and advanced safety locks to ensure operation. They are so fast and versatile that they are a must-have asset for any laboratory or manufacturing plant.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The centrifuge operates quietly and efficiently. It’s compact but surprisingly powerful, making it perfect for daily lab use.
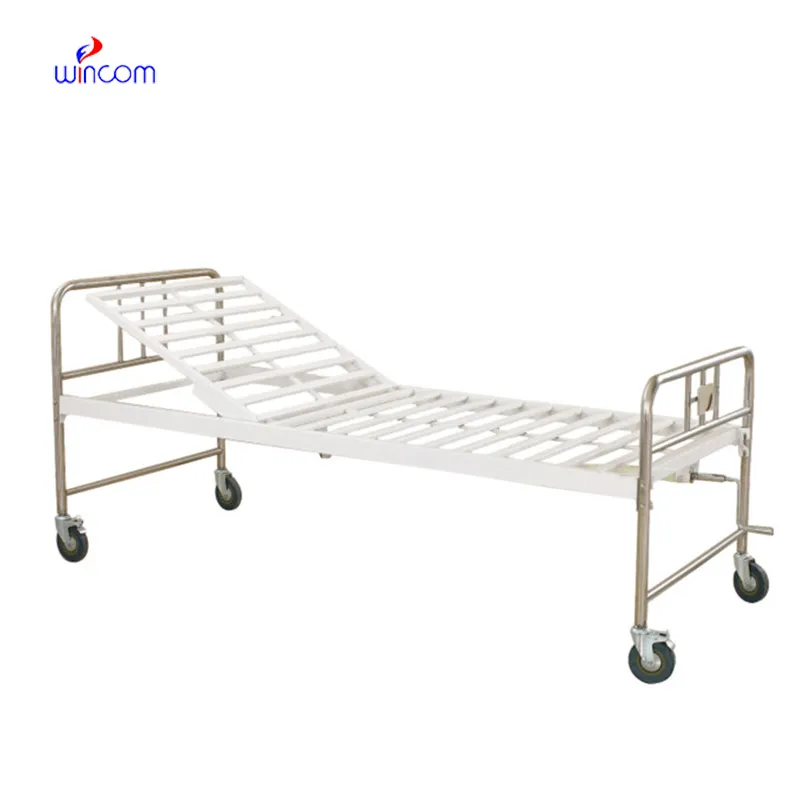
The hospital bed is well-designed and very practical. Patients find it comfortable, and nurses appreciate how simple it is to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
Could you share the specifications and price for your hospital bed models? We’re looking for adjus...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko